Quality Issues
Detect production defects before they impact efficiency and product quality.
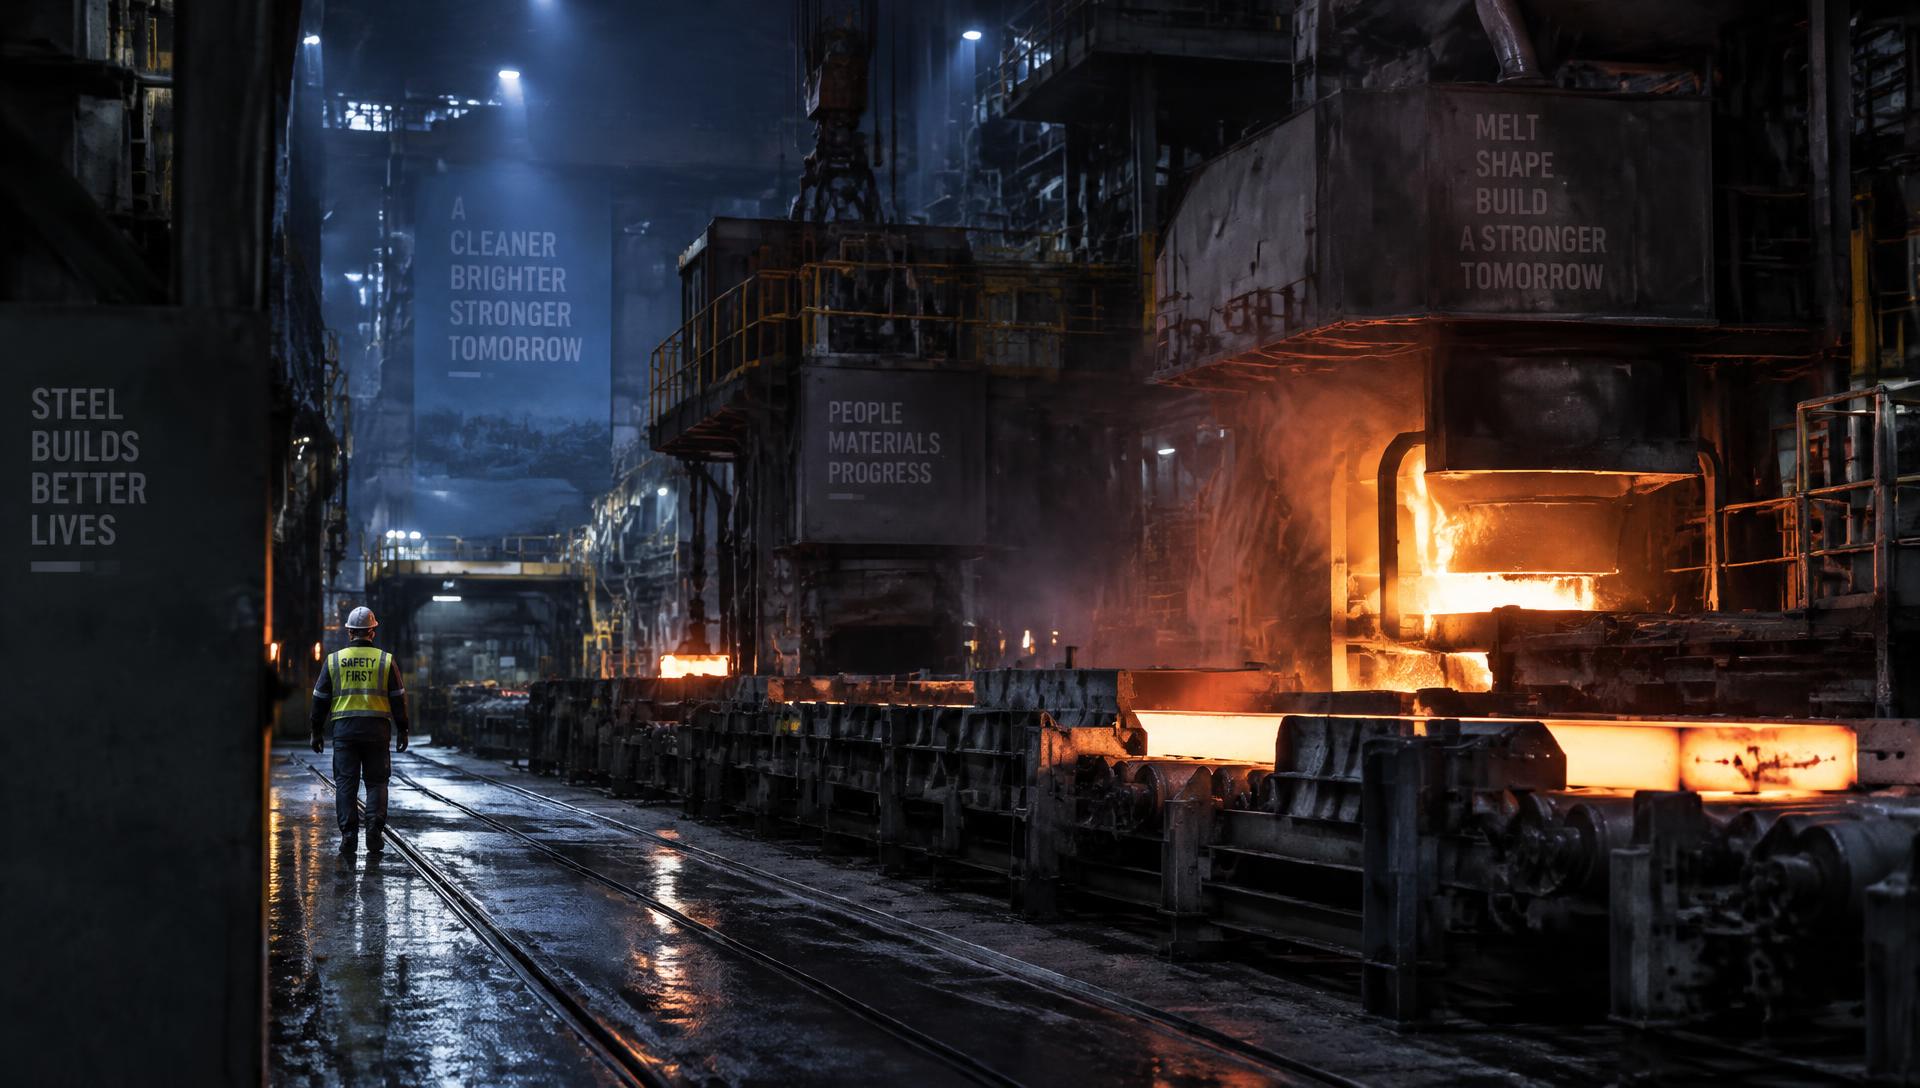
ITP helps industrial companies automate inspections, improve workplace safety, and gain real-time visibility into their operations using advanced AI-powered computer vision technology.
Our solutions are designed around real industrial challenges and help companies reduce risks, improve quality, and make faster decisions.
Industrial facilities generate thousands of hours of visual data every day. However, much of this information remains unused.
ITP transforms camera data into valuable insights that help companies detect problems faster, improve safety, and optimise production processes.
Detect production defects before they impact efficiency and product quality.
Monitor workplace conditions and identify unsafe situations in real time.
Improve visibility and control across industrial processes.
Transform existing cameras into intelligent monitoring systems.
We understand complex industrial environments and develop solutions based on real operational requirements.
Every facility has unique challenges. We create computer vision models adapted to specific processes.
Our solutions can work with current camera systems and industrial infrastructure.
From assessment to deployment and optimisation, we support the entire project lifecycle.
Automatically detect defects during production and improve quality control.
Create safer workplaces with continuous AI-powered monitoring.
Detect early signs of fire and smoke for faster emergency response.
Improve operational visibility using AI analytics.
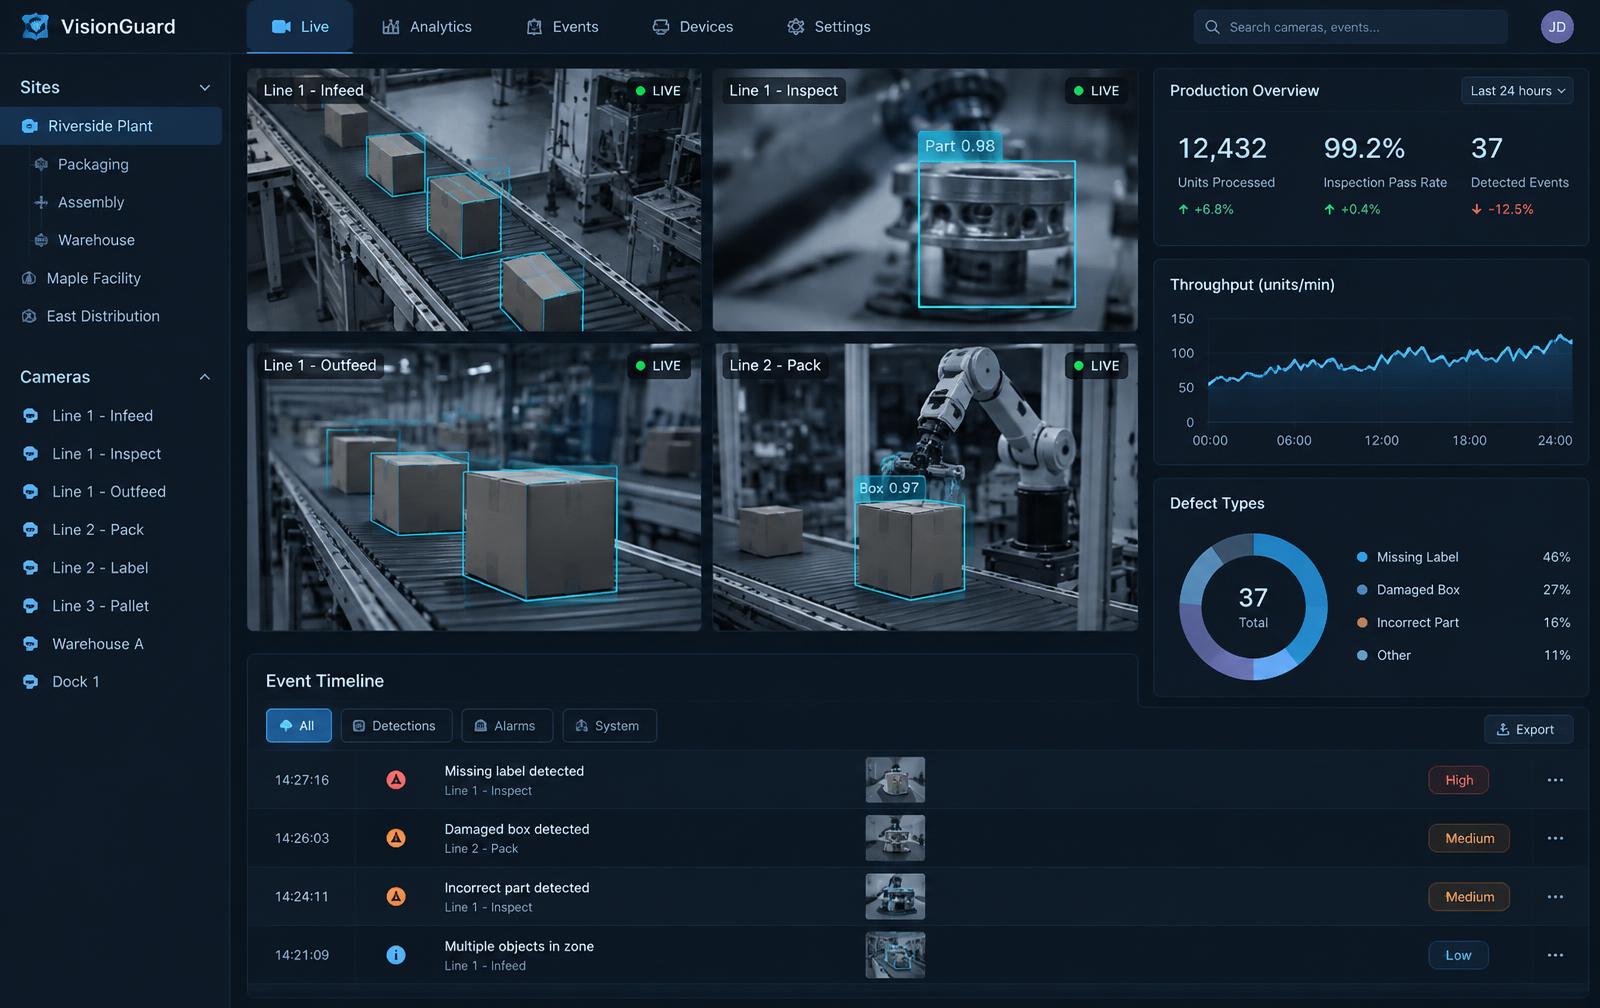
SPAIS is ITP's unified platform for managing computer vision applications from one central environment.
Companies can monitor cameras, manage AI models, analyse events, and expand their computer vision capabilities without creating separate systems.
Challenge
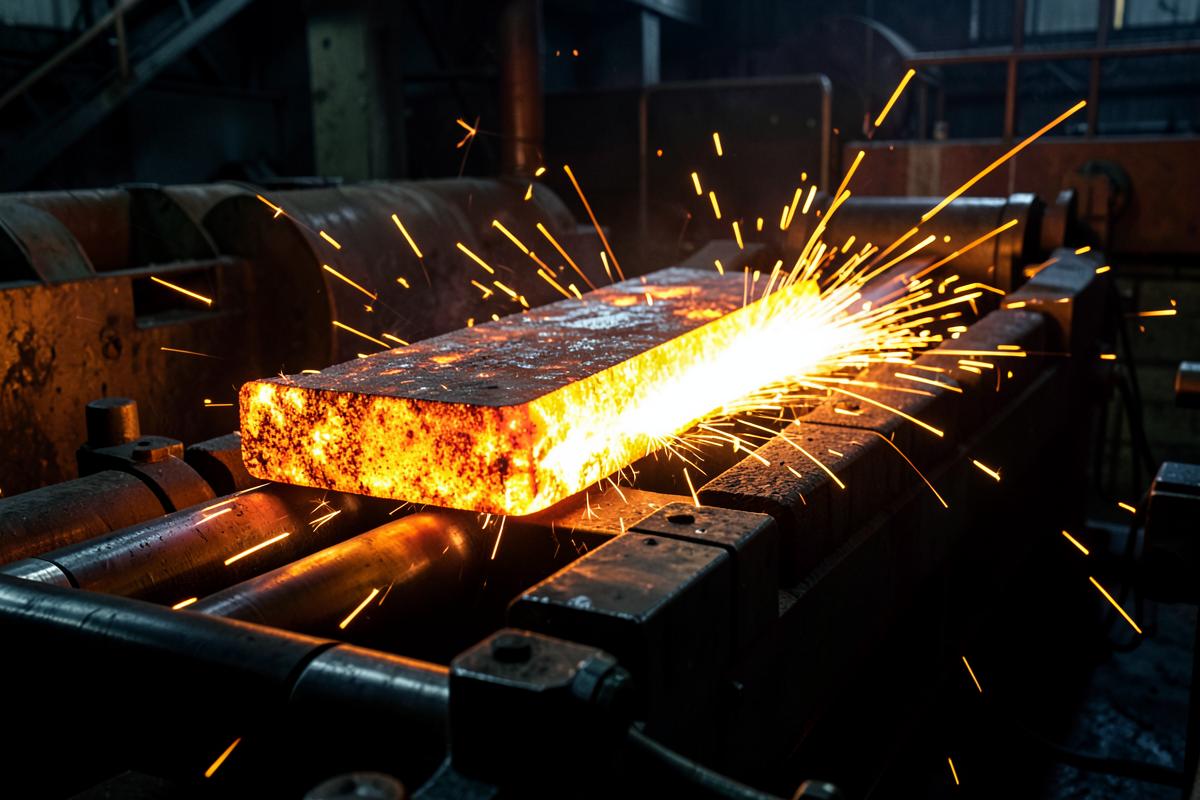
Surface defects during slab production were difficult to identify consistently because of high temperatures and changing surface conditions.
Solution
AI continuously analyses slab surfaces, detects defects, measures their size, and provides operator alerts.
90%
Detection Accuracy
1–2 sec
Response Time
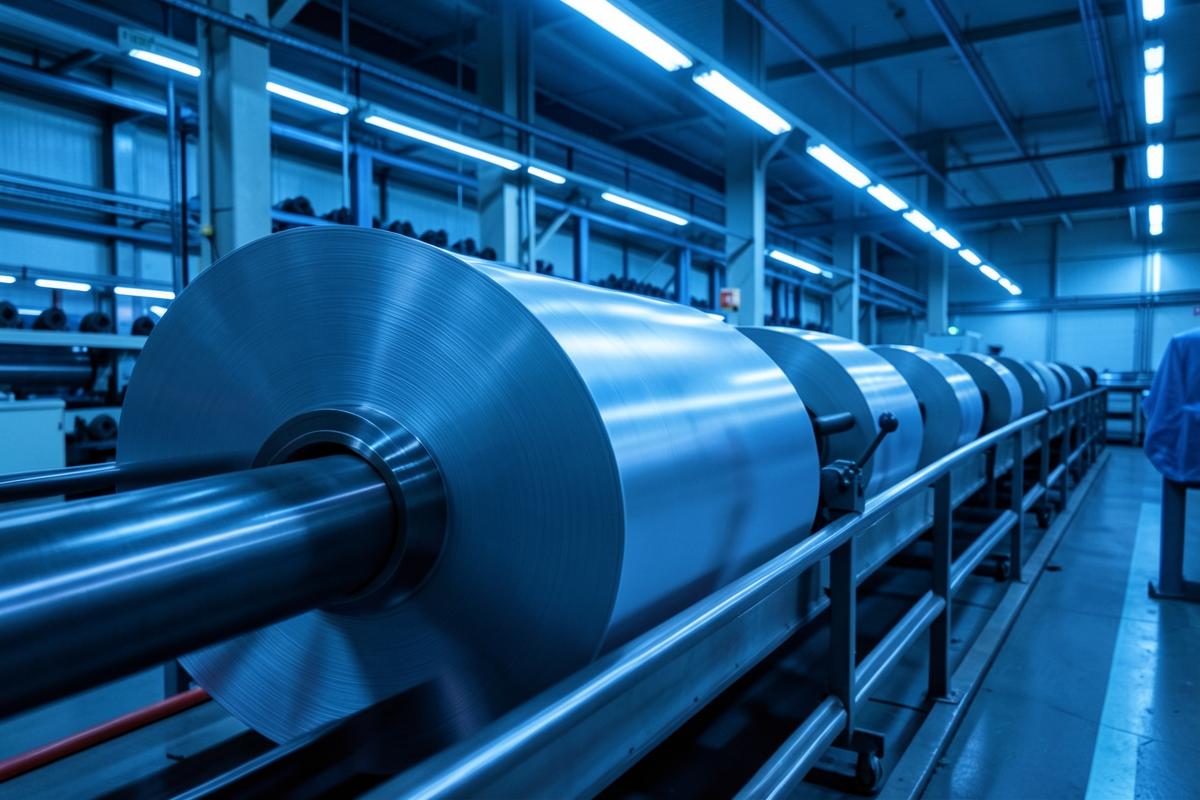
Challenge
High-speed production made manual defect detection difficult.
Solution
Computer vision automatically identifies defects and provides real-time information to operators.
5 m/s
Processing Speed
85%
Detection Accuracy
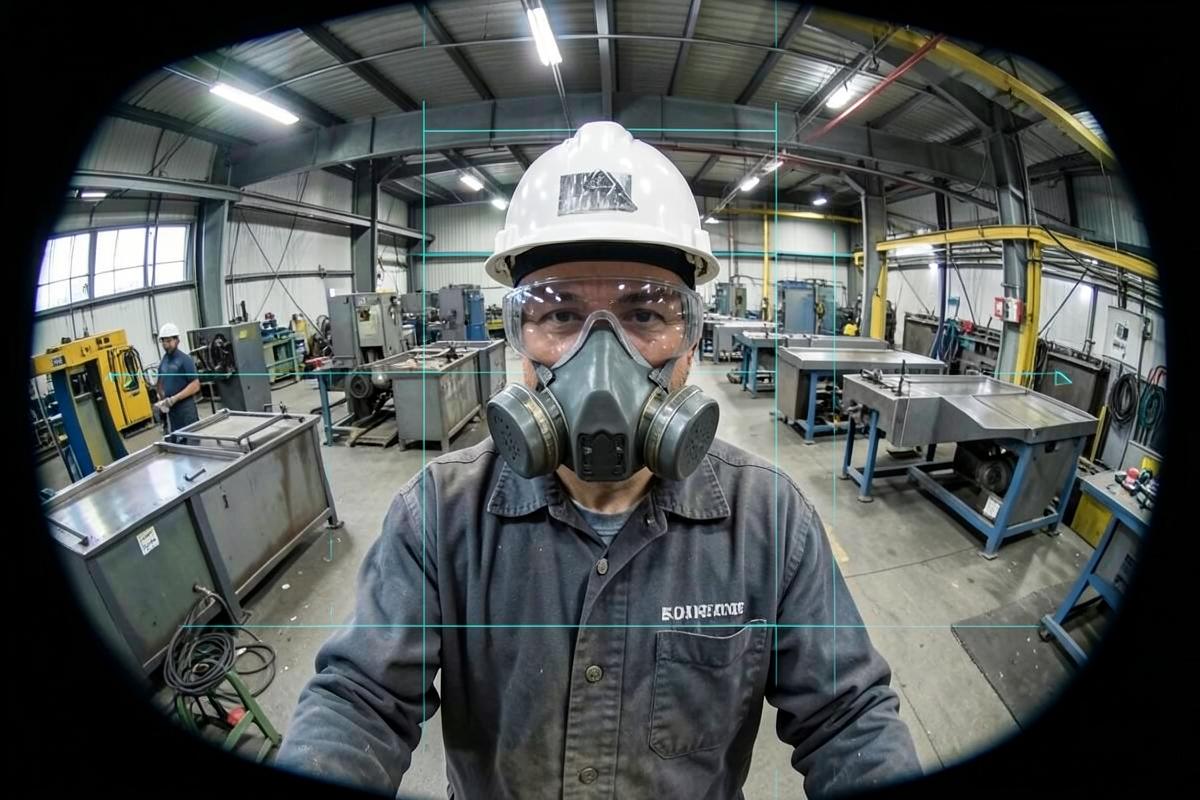
Challenge
Manual safety inspections cannot provide continuous workplace monitoring.
Solution
AI detects whether employees are using required protective equipment.
95%+
Detection Accuracy
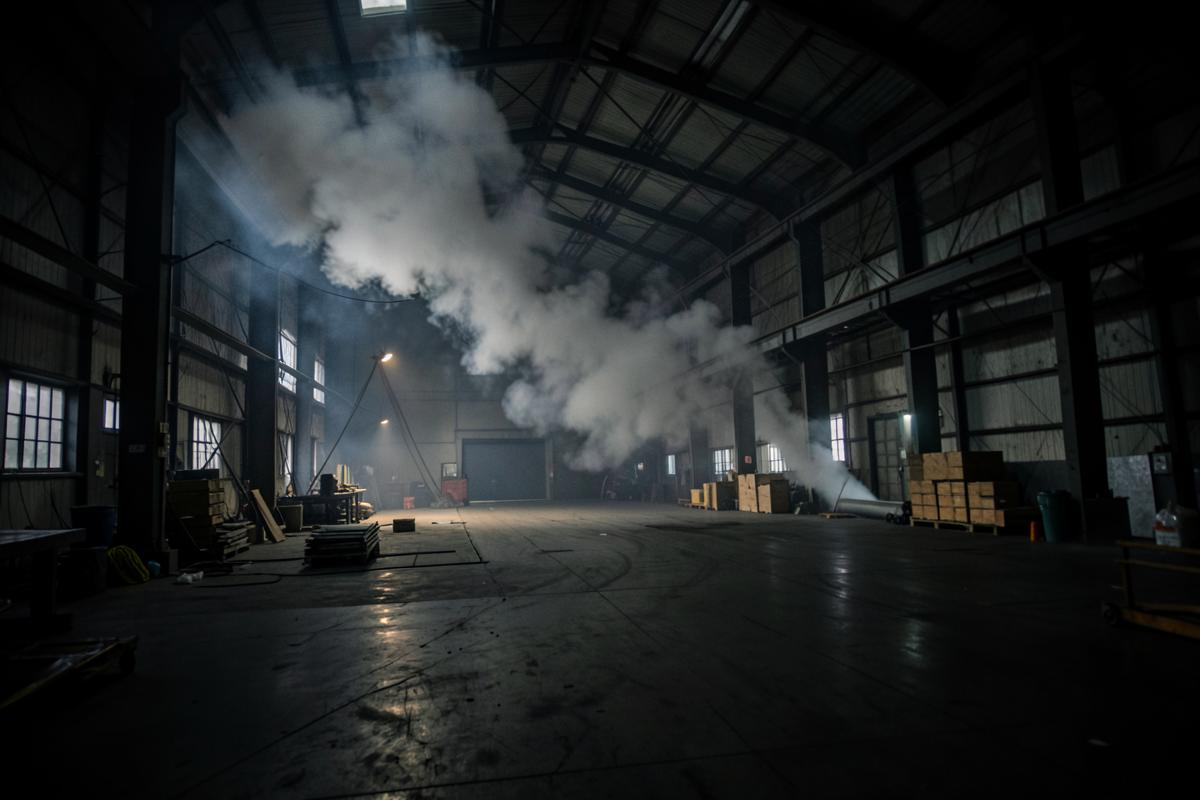
Challenge
Large industrial areas require faster detection than traditional systems.
Solution
AI analyses camera streams and detects smoke and fire at early stages.
30–60 sec
Earlier Detection
Improve safety, monitoring, and operational visibility.
Automate inspection and production control.
Increase quality and reduce manual inspection.
Improve safety and operational management.
Analyse your environment and business objectives.
Create and train models according to your requirements.
Connect with cameras and existing systems.
Continuously optimise results.
Share your industrial challenge and technical setup. Our engineering team will review your case and come back with a feasibility view and a project proposal.
Mining, steel and metallurgy, manufacturing, energy, logistics and any industrial facility with cameras and repeatable visual processes can benefit from computer vision.
In most cases yes. Our solutions are designed to work with current camera systems and industrial infrastructure, so additional hardware is only added when a process requires it.
Accuracy depends on the process and environment. In our industrial projects models typically reach 85–95%+ detection accuracy after training on real production data.
A focused pilot usually takes a few weeks from assessment to first results, while full deployment across multiple lines or sites is planned together with your operations team.
Every model is developed around your specific processes, materials and monitoring zones rather than delivered as a fixed off-the-shelf product.
Yes. We support the entire lifecycle: assessment, model development, integration, deployment, operator training and ongoing optimisation.
Talk with ITP experts and discover how computer vision can help improve safety, quality, and efficiency in your organisation.
Get a Quote